

『Gas Oil Flow Meter In-Line Blending Verification Methods』Related information(v cone flow meter|rotary gas meter|gallon meter|gear meter|metal tube rotameter|glass tube rotameter|nutating disk meter|transit time ultrasonic flow meter|wedge flow meter|pd meters|hydraulic flow meter|ultrasonic water flow meter|water flow meter|air flow meter|magnetic water flow meter|oxygen flow meter|gas flow meter|argon flow meter|air velocity meter|gasoline flow meter|fuel flow meter|ultrasonic water meter|digital water meter|nitrogen flow meter|solid flow meter|Oxygen tank flow meter|digital water flow meter|diesel fuel flow meter|steam flow meter|02 flow meter|compressed air flow meter|oil flow meter|liquid flow meter)
Gas Oil Flow Meter In-Line Blending Verification Methods
Quick Answer: In-line blending verification for gas oil uses a Coriolis mass flow meter placed directly on the blend header. The meter measures real-time density and mass flow and confirms the exact blend ratio, like B10 or B20 biodiesel, without waiting for a lab sample. This method cuts off-spec batches and manual sampling costs at fuel terminals and bunkering stations.
Why Gas Oil Blenders Are Moving to Online Verification
Traditional blend checks rely on taking a sample from a tap, sending it to a lab, and waiting 4 to 24 hours for a result. During that window, a blending skid can push out 200,000 liters of off-spec product before an operator catches the drift. That is a real risk we hear about from fuel depot managers in Malaysia and Nigeria.
An in-line meter eliminates the delay. It scans every liter passing through the pipe. If the density or ratio shifts outside the target band, the PLC gets an alarm signal right away. In practice, a site can switch from corrective action after the fact to preventive control during the blend operation.
Choosing the Right Flow Meter for In-Line Verification
Most engineers start by comparing two sensor types: a positive displacement oval gear meter and a Coriolis mass flow meter. Here is the thing. An oval gear meter gives you volume only. Gas oil volume changes with temperature. A 12 deg C swing in a tank farm in Saudi Arabia or Western Australia can shift the volume by 0.5% or more. You then need a separate densitometer and a PT100 to correct the reading. The cost and calibration effort stack up quickly.
A Coriolis meter from Silver Instruments measures mass flow and live density in one device. You get kg/h and kg/m3 on the same transmitter display. For a B20 diesel verification job, the operator sets a density window, say 830 to 850 kg/m3 at 40 deg C. If the measured density drops below 830, the blend is off spec and the meter triggers a relay output. No extra density meter. No separate flow computer.
For small pipe sizes, a meter with DN15 or DN25 is typical on a single injector line. On a main blend header moving 8,000 kg/h to 15,000 kg/h, a DN50 or DN80 sensor is common. Silver Instruments can supply the meter body in 316L stainless steel, with ATEX Zone 1 or Class I Division 2 approvals for gas oil blending areas.
How the Verification Loop Works in a Typical Gas Oil Rack
Install the meter downstream of the injection point. Keep a straight run of at least 10D upstream and 5D downstream. For a DN50 line, that means 500 mm of straight pipe before the sensor. The meter reports density and mass flow to the PLC via a 4-20 mA HART signal or Modbus RTU.
In a common setup, a base diesel stream runs at 6,000 kg/h and a biodiesel injection pump pushes a small stream through a DN15 line. The Coriolis meter on the combined line reads the final density. The PLC compares the live reading to the recipe density setpoint. When the ratio drifts more than 0.2%, the PLC adjusts the biodiesel pump speed. Operators see the blend ratio update every second on the HMI. There is no grab sample, no lab delay, and no paperwork.
Inline Density Verification Replaces Lab Sampling
Lab sampling is still needed for periodic reference, but daily verification moves to the flow meter. A Coriolis meter with density accuracy of 0.5 kg/m3 can reliably distinguish B10 from neat diesel. That meets the requirement
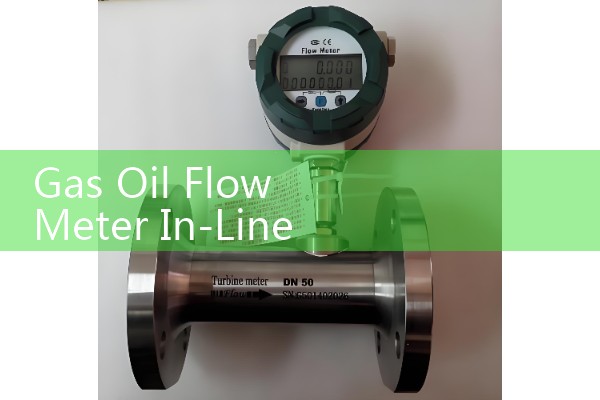
We have seen a customer in Vietnam reduce off-spec events from six times a month to zero after installing a Silver Instruments DN25 Coriolis meter on their B20 skid. The site previously used a turbine meter with a separate densitometer. That combination drifted in the wet monsoon season because the air purge on the densitometer pulled moisture into the sample chamber. The Coriolis single-tube design removed the air purge entirely. You just drain and clean the tube once during a shutdown.
Real Site Check: Verifying B20 in a Southeast Asian Terminal
Last year a fuel terminal in Ho Chi Minh City asked us for a method to verify B20 in-line during truck loading. Their blending skid used an oval gear meter on the biodiesel leg and a turbine meter on the diesel leg. Batch totals matched, but the actual blend ratio drifted by 2% when the diesel temperature rose in the afternoon. They missed a 40,000 liter batch because the lab results arrived the next morning.
We proposed a Silver Instruments Coriolis mass flow meter DN25 on the common discharge header. The meter measured mass flow up to 8,500 kg/h and density in the range of 820 to 860 kg/m3. The output was wired to the existing batch controller. After commissioning, the operator set a density alarm at 838 kg/m3 low limit. The system flagged an alert within 90 seconds of any blend shift. The terminal now validates every truck compartment before the hose is disconnected.
Frequently Asked Questions
Q: What accuracy do I need for in-line gas oil blend verification?
A: For B10 or B20 verification, a mass flow accuracy of 0.15% of rate and a density accuracy of 0.5 kg/m3 is sufficient. That lets you detect a 1% blend ratio change confidently. Silver Instruments standard Coriolis meters meet this spec out of the box.
Q: Can an oval gear meter handle in-line blending verification on its own?
A: No. An oval gear meter measures volume only. You must add a temperature sensor and a density meter to compute mass flow, which adds three calibration points. Many sites prefer a single Coriolis meter to reduce maintenance and avoid drift between separate instruments.
Q: How does the meter handle viscosity changes in gas oil?
A: Coriolis meters measure mass directly and are immune to viscosity shifts between light diesel and heavy gas oil. Oval gear meters need viscosity compensation tables, which often lag real process conditions. That is a key reason blending skids switch to Coriolis technology.
Q: Is a density meter alone sufficient for blend verification?
A: Density alone checks the ratio, but you miss the total mass accountability. A combination mass flow and density meter gives you both the blend ratio and the total mass delivered, which is essential for custody transfer or inventory reconciliation at a fuel terminal.
Q: What data output does Silver Instruments support for blending skids?
A: All meters can output 4-20 mA HART, Modbus RTU, or pulse. For blending skid integration, Modbus RTU over RS485 is the most common pick because it sends density, mass flow, temperature, and totalizer values on a single bus.
Send us your operating pressure (bar), temperature (deg C), pipe size (DN), and target flow range. Our engineers will propose a meter model and verify the straight run requirement for your gas oil blending skid.
 Hot Blog
 Related AD